Skip to content
CNC Programming Hub
  • Home
  • Beginner Guides
  • G-Code & M-Code
  • Machine-Specific
  • Tutorials
  • Resources & Libraries
CNC Programming Hub
  • CNC Alarms

    Fanuc Alarm 130: ILLEGAL AXIS OPERATION

    ByCNC Hub Team October 15, 2026

    Fanuc Alarm 130: ILLEGAL AXIS OPERATION Fanuc Control Model: Fanuc 0i-D/F, 16i/18i/21i and 30i/31i/32i series Fanuc Alarm Description H code and automatic. Have you faced Fanuc Alarm 130 ILLEGAL AXIS OPERATION on your machine? Share your experience or troubleshooting tips in the comments below to help other CNC operators and programmers clear this error faster!
    Read More Fanuc Alarm 130: ILLEGAL AXIS OPERATIONContinue

  • CNC Alarms

    Fanuc Alarm 48: BASIC 3 AXIS NOT FOUND

    ByCNC Hub Team October 15, 2026

    Fanuc Alarm 48: BASIC 3 AXIS NOT FOUND Fanuc Control Model: Fanuc 0i-D/F, 16i/18i/21i and 30i/31i/32i series Fanuc Alarm Description For startup of three–dimensional tool compensation or three–dimensional coordinate conversion, the three basic axes used when Xp,Yp and Zp are omitted were not specified in parameter No. 1022. Have you faced Fanuc Alarm 48 BASIC…

    Read More Fanuc Alarm 48: BASIC 3 AXIS NOT FOUNDContinue

  • CNC Alarms

    Fanuc Alarm 124: MISSING END STATEMENT

    ByCNC Hub Team October 15, 2026

    Fanuc Alarm 124: MISSING END STATEMENT Fanuc Control Model: Fanuc 0i-D/F, 16i/18i/21i and 30i/31i/32i series Fanuc Alarm Description DO – END does not correspond to 1: 1. Modify the program. Have you faced Fanuc Alarm 124 MISSING END STATEMENT on your machine? Share your experience or troubleshooting tips in the comments below to help other…

    Read More Fanuc Alarm 124: MISSING END STATEMENTContinue

  • CNC Alarms

    Fanuc Alarm 80: G37 ARRIVAL SIGNAL NOT ASSERTED

    ByCNC Hub Team October 15, 2026

    Fanuc Alarm 80: G37 ARRIVAL SIGNAL NOT ASSERTED Fanuc Control Model: Fanuc 0i-D/F, 16i/18i/21i and 30i/31i/32i series Fanuc Alarm Description M series In the automatic tool length measurement function (G37), the measurement position reach signal (XAE, YAE,or ZAE) is not turned on within an area specified in parameter 6254 (value ε).This is due to a…

    Read More Fanuc Alarm 80: G37 ARRIVAL SIGNAL NOT ASSERTEDContinue

  • G95 Feed Per Revolution in CNC Programming
    Beginner Guides | G-Code & M-Code

    G95 Feed Per Revolution in CNC Programming

    ByCNC Hub Team October 13, 2026

    Various G-Codes are used to control feed rates in CNC machines. Among them, G95 Feed Per Revolution is an important command, which controls the feed rate per spindle revolution.This code links the feed rate to the spindle speed, and this is the basis for a better surface finish and longer tool life. G95 stands for…

    Read More G95 Feed Per Revolution in CNC ProgrammingContinue

  • Fanuc G21: Programming a CNC Lathe in Millimeters
    Beginner Guides | G-Code & M-Code

    Fanuc G21: Programming a CNC Lathe in Millimeters

    ByCNC Hub Team October 11, 2026October 11, 2026

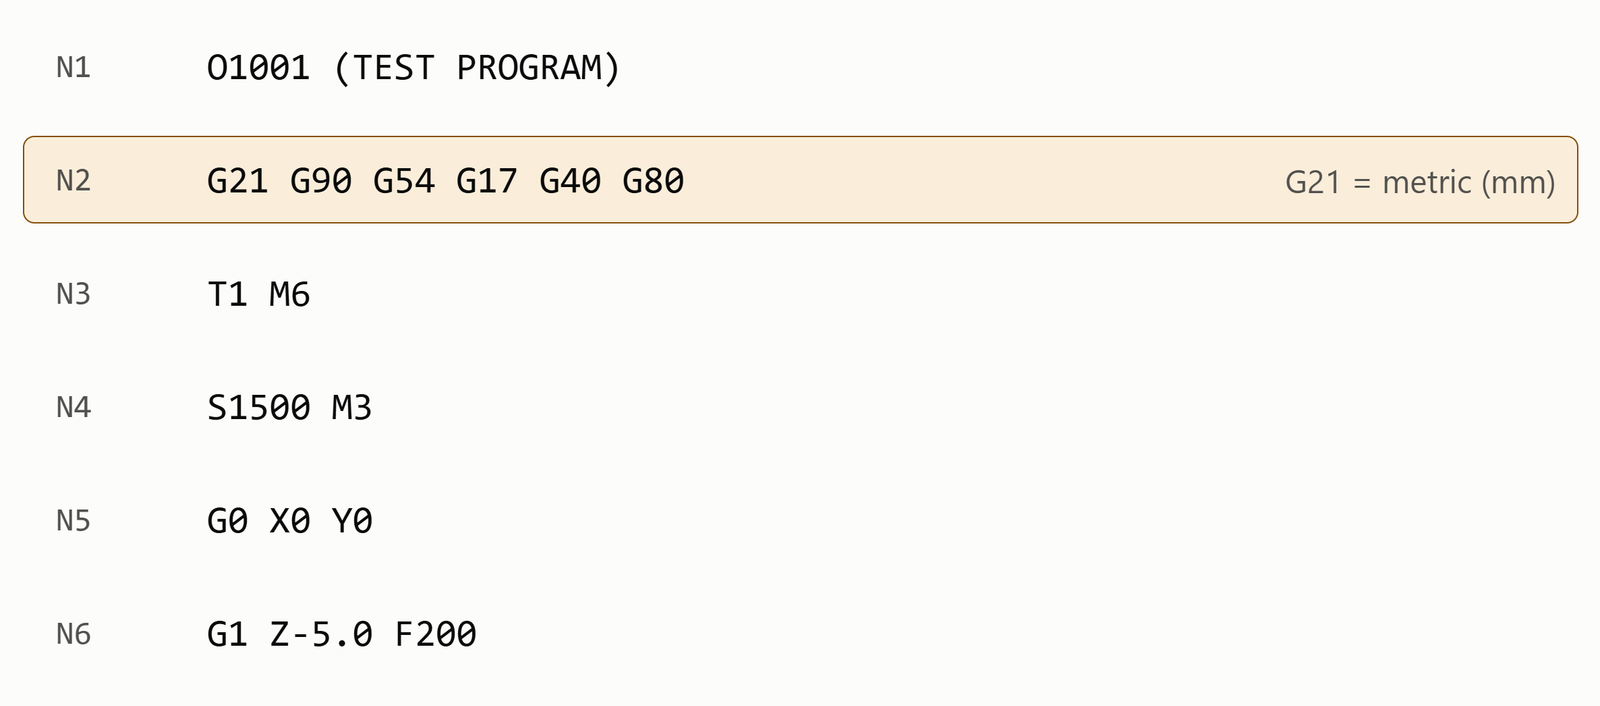
    G21 is a G-Code command that tells the CNC machine that all positions, distances, and feed rates should now be understood in metric units (millimeters). When G21 is used, the CNC machine understands all relevant linear measurements in millimeters (mm). G21 = Metric mode (millimeters, and feeds in mm/min or mm/rev)G20 = Inch mode (its…

    Read More Fanuc G21: Programming a CNC Lathe in MillimetersContinue

  • M08 and M09 CNC Codes
    G-Code & M-Code

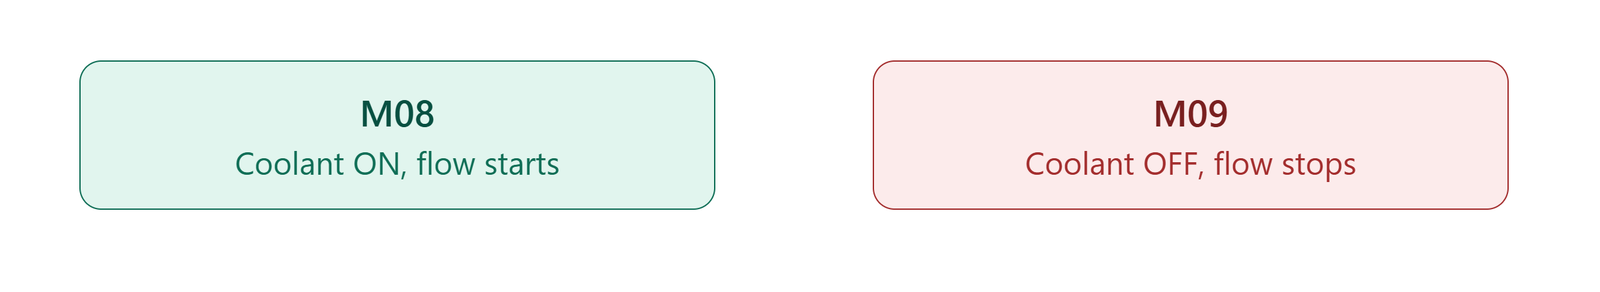
    M08 and M09 CNC Codes: Coolant ON and OFF Commands

    ByCNC Hub Team October 10, 2026October 10, 2026

    The use of coolant is very important for the safety of the tool (Tool Life), and for the best cutting while working on the machine. The correct use of coolant has a direct impact on the life of the tool, surface finish and machine performance.During machining, a lot of heat is generated due to friction…

    Read More M08 and M09 CNC Codes: Coolant ON and OFF CommandsContinue

  • G00 Rapid Traverse in CNC Programming: Complete Guide & Examples
    G-Code & M-Code

    G00 Rapid Traverse in CNC Programming: Complete Guide & Examples

    ByCNC Hub Team October 7, 2026

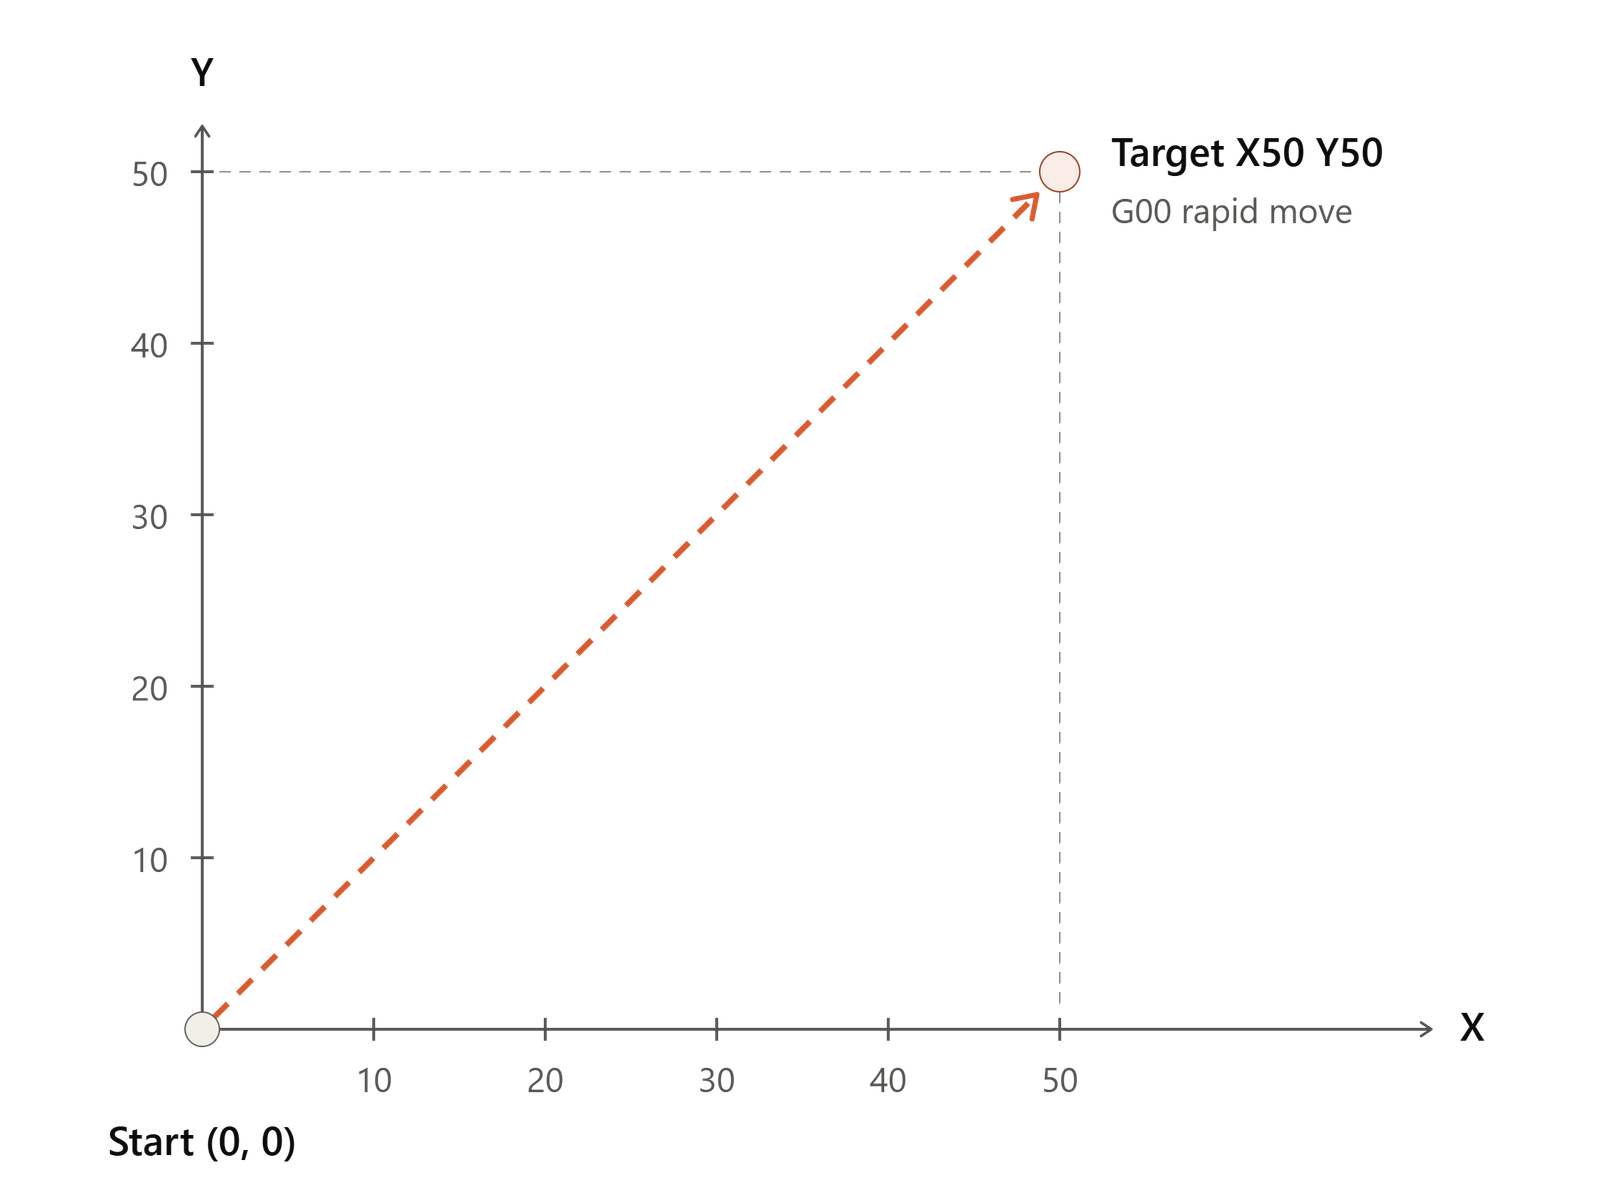
    One of the codes that must be learned before working on a CNC machine is G00. This command moves the tool from one point to another very quickly. In this, the tool does not cut, but only changes its positioning. In CNC programming, this command is used to move the tool from one point to…

    Read More G00 Rapid Traverse in CNC Programming: Complete Guide & ExamplesContinue

  • Step Turning CNC Lathe Programming
    Tutorials

    Step Turning CNC Lathe Programming Guide with G-Code Example

    ByCNC Hub Team October 6, 2026October 6, 2026

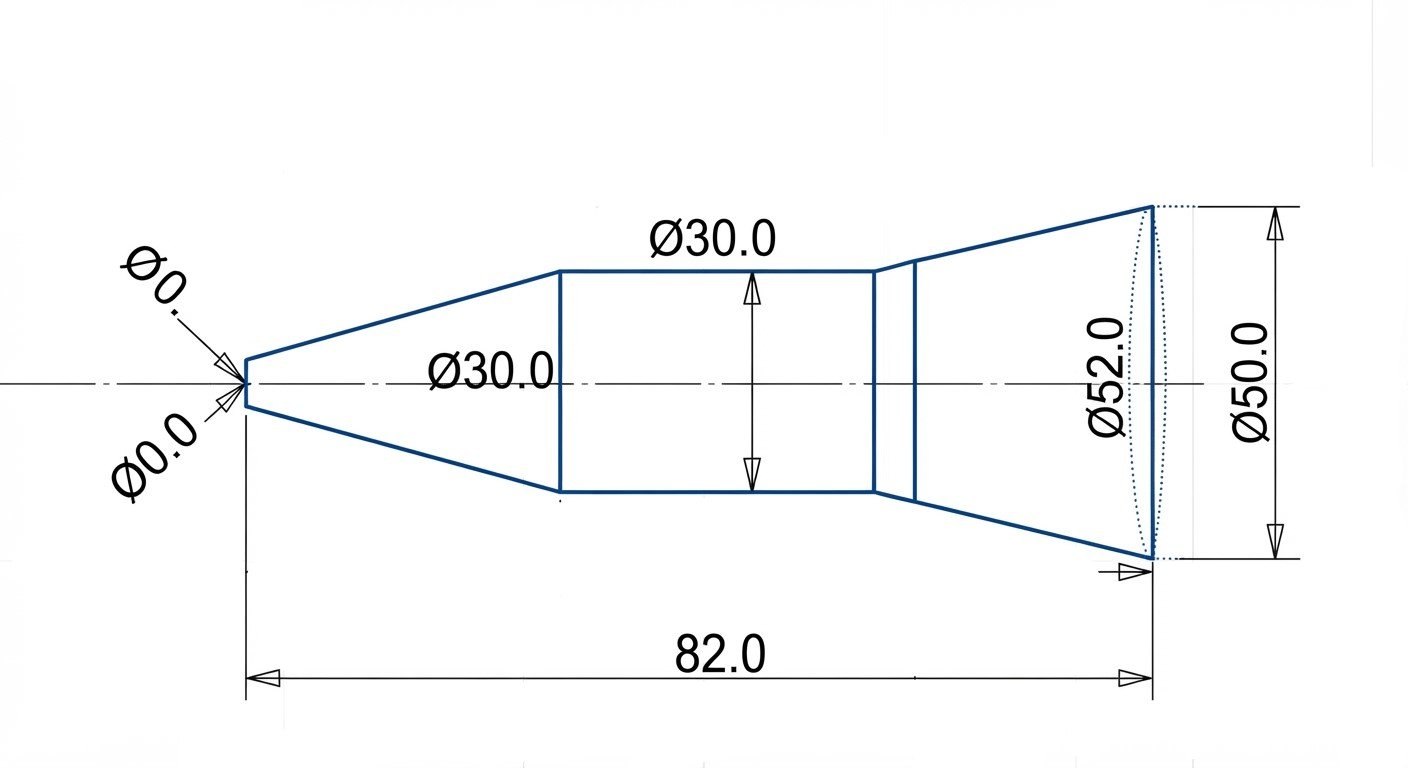
    In step turning, different parts of a cylindrical workpiece are turned to different diameters. The finished component therefore includes two or more diameter or “steps”. Step Turning CNC Lathe Programming Example This program is for Step Turning / Taper Turning on a CNC Lathe. It will create a cylindrical job with a stepped profile with…

    Read More Step Turning CNC Lathe Programming Guide with G-Code ExampleContinue

  • CNC Lathe Taper Turning Program Using G01 Linear Interpolation
    G-Code & M-Code

    CNC Lathe Taper Turning Program Using G01 Linear Interpolation

    ByCNC Hub Team October 6, 2026October 6, 2026

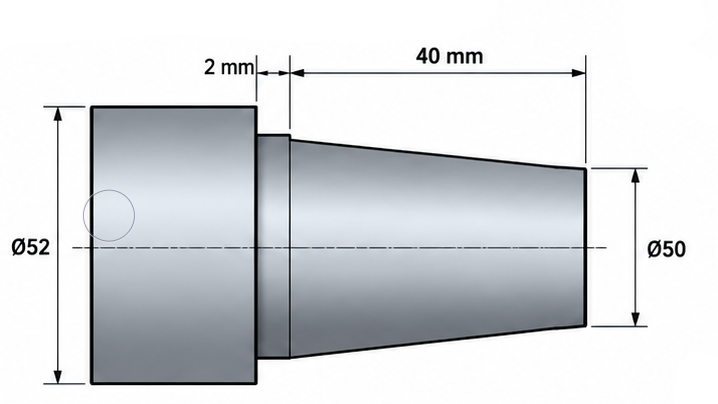
    Starting diameter: Ø50 mm Taper end diameter: Ø30 mm Taper length: 40 mm Related: Turning & Arc Interpolation (G03) Main Machining Operations (N50 – N80) Program Sequence This is a simple and clean program for CNC Lathe. It moves the tool to the position exactly in front of the workpiece, then performs Facing and a…

    Read More CNC Lathe Taper Turning Program Using G01 Linear InterpolationContinue

  • CNC Lathe G33 Threading Program Example
    Beginner Guides | Tutorials

    CNC Lathe G33 Threading Program Example (Single-Pass Threading)

    ByCNC Hub Team October 4, 2026

    The following CNC lathe program demonstrates a simple external threading operation using the G33 threading cycle. In this example, the CNC lathe cuts an M20 × 2.0 metric thread over a 30 mm length in a single threading pass. This program is intentionally kept very simple and uses a single threading pass without multiple cutting…

    Read More CNC Lathe G33 Threading Program Example (Single-Pass Threading)Continue

  • G74 for Deep-Hole Drilling on a CNC Lathe
    G-Code & M-Code

    How to Use G74 for Deep-Hole Drilling on a CNC Lathe

    ByCNC Hub Team October 4, 2026October 4, 2026

    This CNC program is designed for a drilling operation on a workpiece, using a peck-drilling cycle to create a 60 mm deep hole along the Z-axis. O0001 — G74 PECK DRILLING EXAMPLEN10 G21 G99 — Metric units; feed in mm/revolutionN20 T0505 M06 — Select drill tool, tool offset 05N30 G97 S800 M03 — Spindle ONN40…

    Read More How to Use G74 for Deep-Hole Drilling on a CNC LatheContinue

  • CNC Pocket Milling Program Example
    Tutorials

    Short CNC Pocket Milling Program Example and Explanation

    ByCNC Hub Team October 4, 2026October 9, 2026

    CNC Pocket Milling is a very important process. It is a process in which a specific depth of a box, cavity or hole (Pocket) is cut out by a CNC machine inside a metal block (Workpiece). In simple words, its purpose is to empty the interior of a material to a specific shape and depth,…

    Read More Short CNC Pocket Milling Program Example and ExplanationContinue

  • Haas

    Haas Alarm: 187 B SERVO ERROR TOO LARGE – Mill

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 187 B SERVO ERROR TOO LARGE – Mill Haas Alarm Description Too much load or speed on B-axis motor. The difference between the motor position and the commanded position has exceeded Parameter 159. The motor may also be stalled, disconnected, or the driver failed. The servos will be turned off and a Reset…

    Read More Haas Alarm: 187 B SERVO ERROR TOO LARGE – MillContinue

  • Haas

    Haas Alarm: 187 B SERVO ERROR TOO LARGE – Lathe

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 187 B SERVO ERROR TOO LARGE – Lathe Haas Alarm Description Too much load or speed on B-axis motor. The difference between the motor position and the commanded position has exceeded a parameter. The motor may also be stalled, disconnected, or the driver failed. The servos will be turned off and a Reset…

    Read More Haas Alarm: 187 B SERVO ERROR TOO LARGE – LatheContinue

  • Haas

    Haas Alarm: 186 SPINDLE NOT TURNING

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 186 SPINDLE NOT TURNING Haas Alarm Description The spindle is not turning; check your program for G99 Feed Per Revolution or G98 Feed Per Minute. References Haas CNC Alarms and Troubleshooting by official Haas Automation documentation. Have you faced Haas Alarm 186 SPINDLE NOT TURNING  on your machine? Share your experience or troubleshooting tips…

    Read More Haas Alarm: 186 SPINDLE NOT TURNINGContinue

  • Haas

    Haas Alarm: 185 A CABLE FAULT

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 185 A CABLE FAULT Haas Alarm Description Cable from A-axis encoder does not have valid differential signals. References Haas CNC Alarms and Troubleshooting by official Haas Automation documentation. Have you faced Haas Alarm 185 A CABLE FAULT  on your machine? Share your experience or troubleshooting tips in the comments below to help other CNC…

    Read More Haas Alarm: 185 A CABLE FAULTContinue

  • Haas

    Haas Alarm: 184 Z CABLE FAULT

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 184 Z CABLE FAULT Haas Alarm Description Cable from Z-axis encoder does not have valid differential signals. References Haas CNC Alarms and Troubleshooting by official Haas Automation documentation. Have you faced Haas Alarm 184 Z CABLE FAULT  on your machine? Share your experience or troubleshooting tips in the comments below to help other CNC…

    Read More Haas Alarm: 184 Z CABLE FAULTContinue

  • Haas

    Haas Alarm: 183 Y CABLE FAULT – Mill

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 183 Y CABLE FAULT – Mill Haas Alarm Description Cable from Y-axis encoder does not have valid differential signals. References Haas CNC Alarms and Troubleshooting by official Haas Automation documentation. Have you faced Haas Alarm 183 Y CABLE FAULT – Mill  on your machine? Share your experience or troubleshooting tips in the comments below…

    Read More Haas Alarm: 183 Y CABLE FAULT – MillContinue

  • Haas

    Haas Alarm: 183 LIVE TOOLING CABLE FAULT – Lathe

    ByCNC Hub Team October 3, 2026October 3, 2026

    Haas Alarm: 183 LIVE TOOLING CABLE FAULT– Lathe Haas Alarm Description Cable from Live Tooling motor encoder does not have valid differential signals. References Haas CNC Alarms and Troubleshooting by official Haas Automation documentation. Have you faced Haas Alarm 183 LIVE TOOLING CABLE FAULT – Lathe  on your machine? Share your experience or troubleshooting tips in…

    Read More Haas Alarm: 183 LIVE TOOLING CABLE FAULT – LatheContinue

Page navigation

1 2 3 … 20 Next PageNext
  • About Us – CNC Programming Hub
  • Contact Us
  • Privacy Policy

© 2026 CNC Programming Hub

  • Home
  • Beginner Guides
  • G-Code & M-Code
  • Machine-Specific
  • Tutorials
  • Resources & Libraries
Search