CNC Lathe Facing Program – Fanuc G Code Step by Step
Facing is a basic machining operation performed on a CNC lathe, the purpose of which is to cut the end face of a workpiece to a perfectly smooth, straight, and accurate length.
The main purpose of facing in a CNC machine is to make the end of the workpiece perfectly smooth, clean and straight so that an accurate and parallel reference surface can be obtained for all subsequent machining or cutting.
When raw material is clamped in a chuck, its cut end is often uneven or rough. This operation removes excess material from this surface and makes it perfectly perpendicular to the axis of the tool.
Sample CNC Lathe Facing Program (G-Code Example)
Here is a standard G-code program snippet for a facing operation on a CNC lathe (Fanuc controller compatible):
O1001 (CNC LATHE FACING PROGRAM)
G21 G40 G99 G18
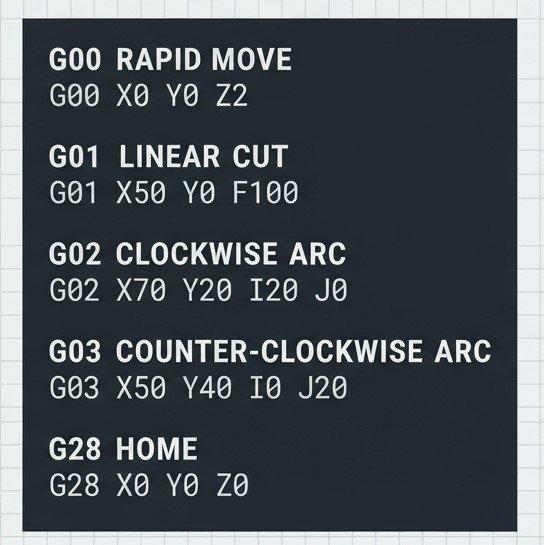
G28 U0 W0
T0101 (FACING TOOL)
G97 S1200 M03
G00 X52.0 Z2.0 M08
G01 Z0.0 F0.15
X-1.0 F0.1
G00 Z2.0
G28 U0 W0
M30
Program Explanation
O1001 (CNC LATHE FACING PROGRAM)
- This is the program number, which saves the program in the machine.
G21 G40 G99 G18
- G21: All measurements are in millimeters (mm).
- G40: Tool Radius Compensation Cancel.
- G99: Feed rate per revolution (Feed per Revolution – mm/rev).
- G18: ZX plane selection (working on Z and X axes).
G28 U0 W0
- Returns the tool to its home position.
T0101 (FACING TOOL)
- Selects tool number 1 and its offset number 1.
G97 S1200 M03
- G97: Constant speed mode (Constant Surface Speed off).
- S1200: Spindle speed 1200 RPM.
- M03: Spindle forward.
G00 X52.0 Z2.0 M08
- The tool approaches the job quickly (52 mm on X and 2 mm on Z).
- M08: Turns on the coolant.
G01 Z0.0 F0.15
- The cutting begins (Facing cut). The tool moves to Z=0 (face of the job) and the feed rate is 0.15 mm per revolution.
X-1.0 F0.1
- The tool moves slightly beyond the center (X = -1.0) to completely cut the face so that there is no mark in the middle.
G00 Z2.0
- After cutting, the tool quickly retracts (to Z = 2.0).
G28 U0 W0
- All axes of the machine (X and Z) return to their home positions.
M30
- End of program and rewind.