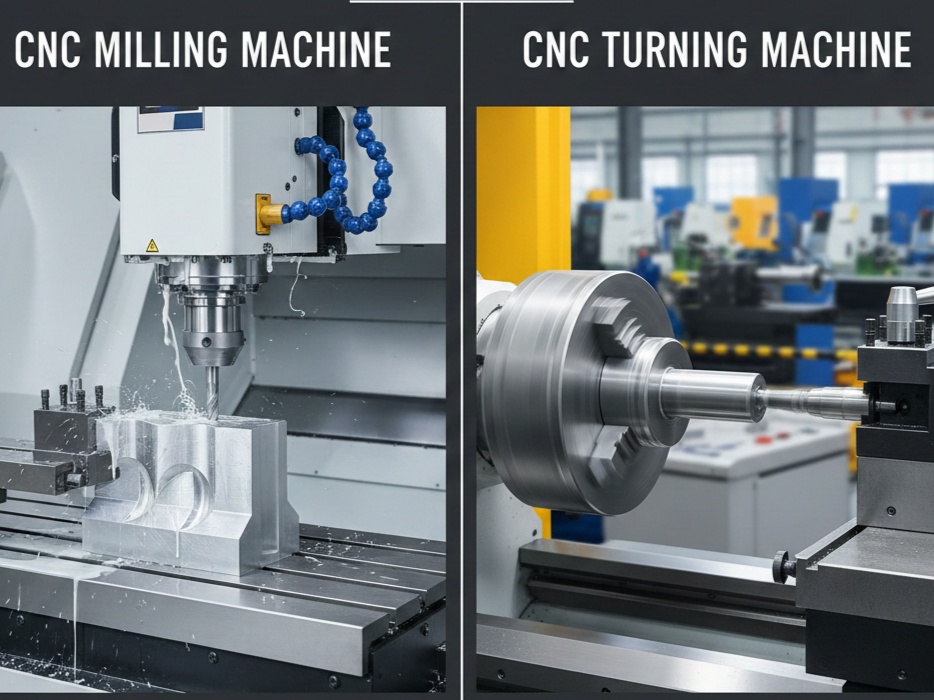
G95 Feed Per Revolution in CNC Programming
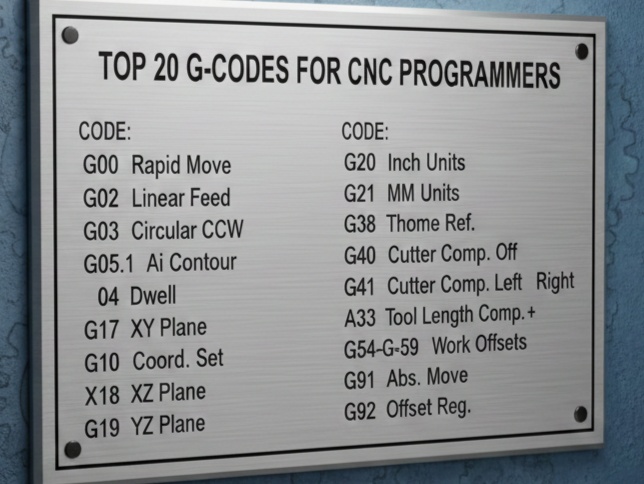
Various G-Codes are used to control feed rates in CNC machines. Among them, G95 Feed Per Revolution is an important command, which controls the feed rate per spindle revolution.
This code links the feed rate to the spindle speed, and this is the basis for a better surface finish and longer tool life.
G95 stands for Feed Per Revolution, which is how much the tool will move in each revolution of the spindle. Its unit is usually millimeters per revolution (mm/rev) or inches per revolution (in/rev).
For example, F0.2 means that the tool will move 0.2 mm for each revolution of the spindle.
What is G95 Feed Per Revolution?
G95 is a modal command that sets the feed rate per revolution of the spindle.
This means that the program specifies the feed rate, which is the distance the tool will travel during one complete revolution of the spindle.
For example:
G95 F0.20The above is the G-code for a CNC machine (lathe/turning center).
F0.20. With G95 this means that the tool will move 0.20 mm forward for each spindle revolution (if the machine is in metric mode).
If the spindle is rotating at 1000 RPM, the feed rate will be approximately 1000 × 0.20 = 200 mm/min. The feed rate automatically changes proportionally when the spindle speed changes.
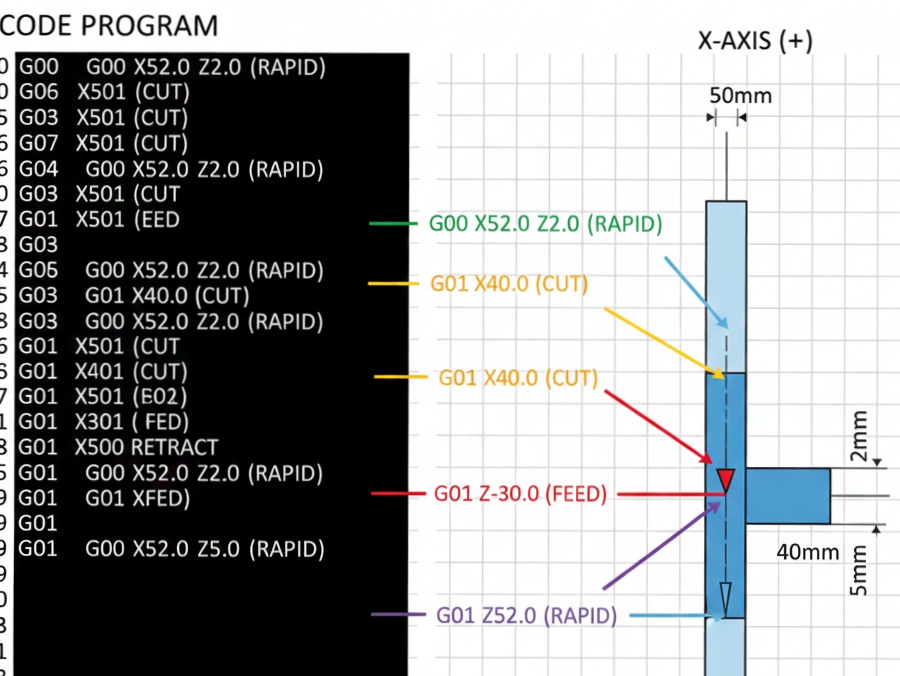
Program Example (Turning)
G21 G40 G95
T0101
G96 S180 M03
G50 S2500
G00 X52.0 Z2.0
G01 Z-40.0 F0.25
G01 X56.0
G00 X100.0 Z100.0
M30
Differences according to machine control
- Fanuc (milling): G94 is for minutes at feed and G95 is for revolutions at feed.
- Fanuc (lathe): Some models use G98 and G99, while others use G94 and G95. This depends on the parameter or type of control.
- Siemens: G94: and G95 generally do the same thing.
Be sure to check your machine manual, as incorrect codes can cause the machine to run at unexpected speeds.