CNC Lathe Taper Turning Program Using G01 Linear Interpolation
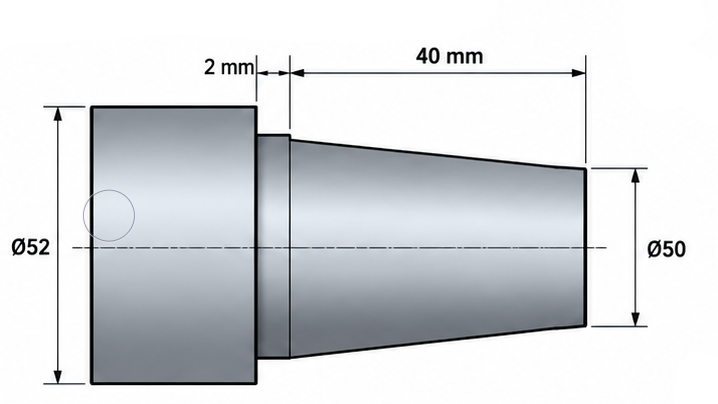
Starting diameter: Ø50 mm Taper end diameter: Ø30 mm Taper length: 40 mm
Related: Turning & Arc Interpolation (G03)
O0100

N10 G21 G40 G99
N20 T0101
N30 G97 S800 M03
N40 M08

N50 G00 X52.0 Z2.0
N60 G01 Z0.0 F0.20
N70 G01 X45.0 Z0.0
N80 G01 X50.0 Z-40.0

N90 G00 X55.0 Z5.0
N100 M09
N110 M05
N120 M30
Main Machining Operations (N50 – N80)
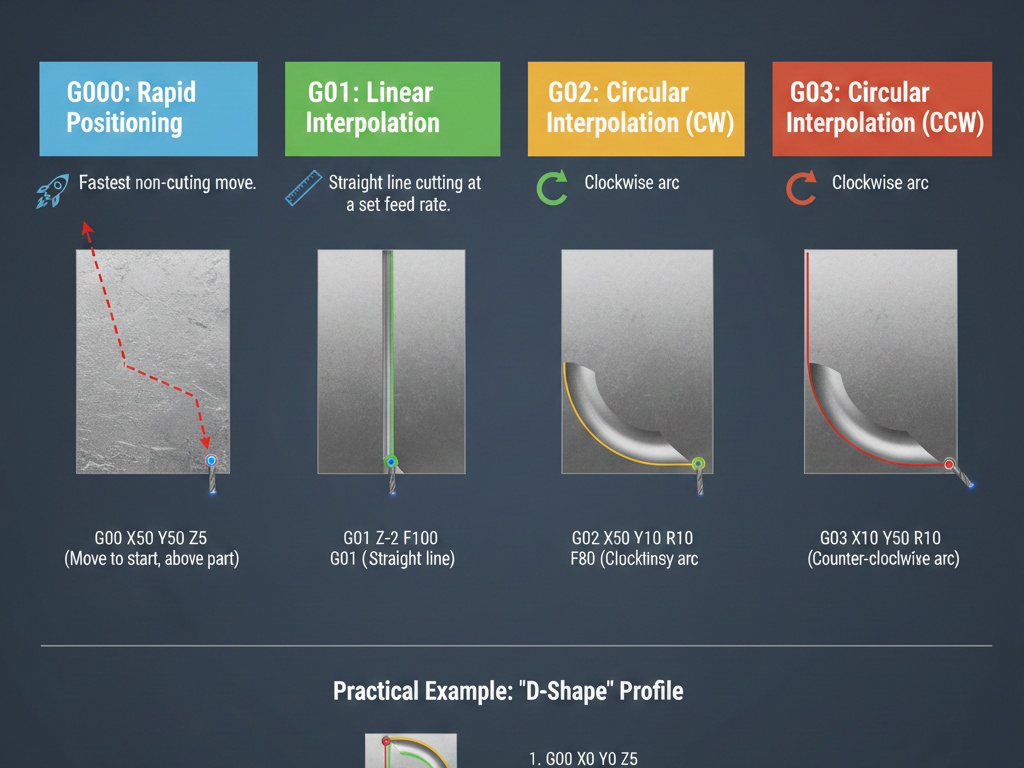
- N50 G00 X52.0 Z2.0: Rapid traverse (G00) to a safe approach position just clear of the workpiece outer diameter ($X=52$ mm, $Z=2$ mm).
- N60 G01 Z0.0 F0.20: Linear feed (G01) forward to the face of the part at $Z = 0.0$ with a feed rate of 0.20 mm/rev.
- N70 G01 X45.0 Z0.0: Faces inward across the part face down to $X = 45.0$ mm.
- N80 G01 X50.0 Z-40.0: Performs a linear cut moving diagonally (taper/chamfer/turning transition) up to $X = 50.0$ mm and a depth of $Z = -40.0$ mm.
Program Sequence
This is a simple and clean program for CNC Lathe. It moves the tool to the position exactly in front of the workpiece, then performs Facing and a simple Turning operation. Below is the description of each line.
| Block | Code | Operation |
|---|---|---|
| N10 | G21 G40 G99 | Set metric units, cancel cutter compensation, and set feed-per-revolution mode |
| N20 | T0101 | Select Tool 1 with Offset 1 |
| N30 | G97 S800 M03 | Set constant spindle speed to 800 RPM and start spindle clockwise |
| N40 | M08 | Turn coolant ON |
| N50 | G00 X52.0 Z2.0 | Rapidly position tool near the workpiece |
| N60 | G01 Z0.0 F0.20 | Feed tool to the Z0 face at 0.20 mm/rev |
| N70 | G01 X45.0 Z0.0 | Move in X to Ø45 mm while remaining at Z0 — this performs the facing cut |
| N80 | G01 X50.0 Z-40.0 | Feed diagonally from Ø45/Z0 to Ø50/Z-40 |
| N90 | G00 X55.0 Z5.0 | Rapidly retract tool to a safe position |
| N100 | M09 | Coolant OFF |
| N110 | M05 | Spindle OFF |
| N120 | M30 | End program |