How to Use G74 for Deep-Hole Drilling on a CNC Lathe
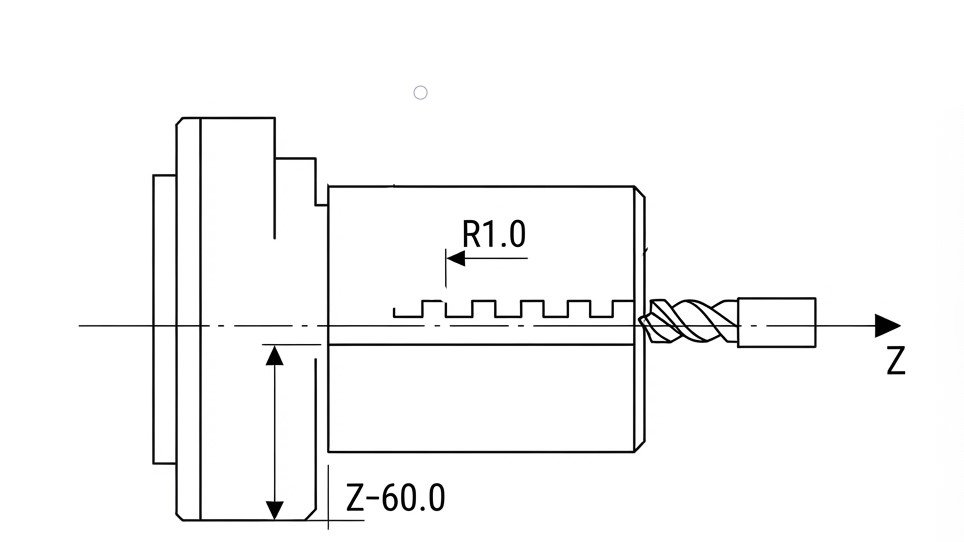
This CNC program is designed for a drilling operation on a workpiece, using a peck-drilling cycle to create a 60 mm deep hole along the Z-axis.
O0001
N10 G21 G99
N20 T0505 M06
N30 G97 S800 M03
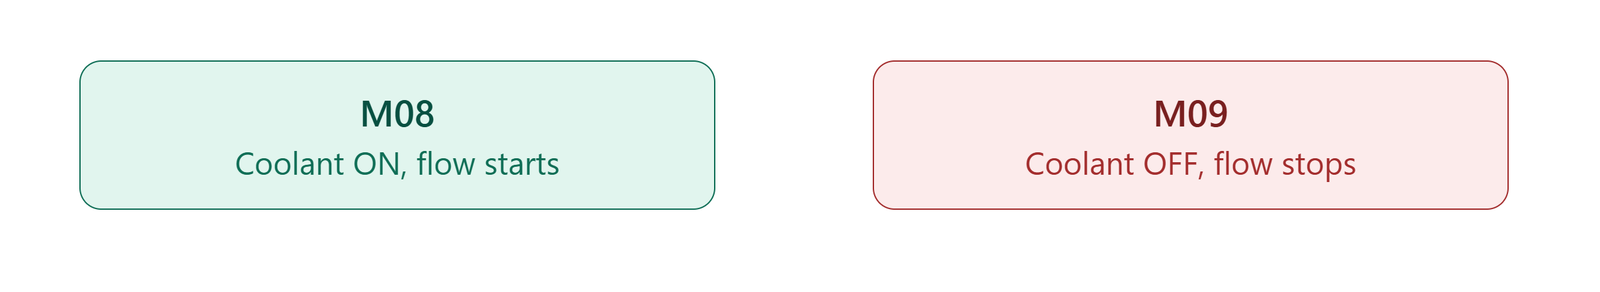
N40 M08
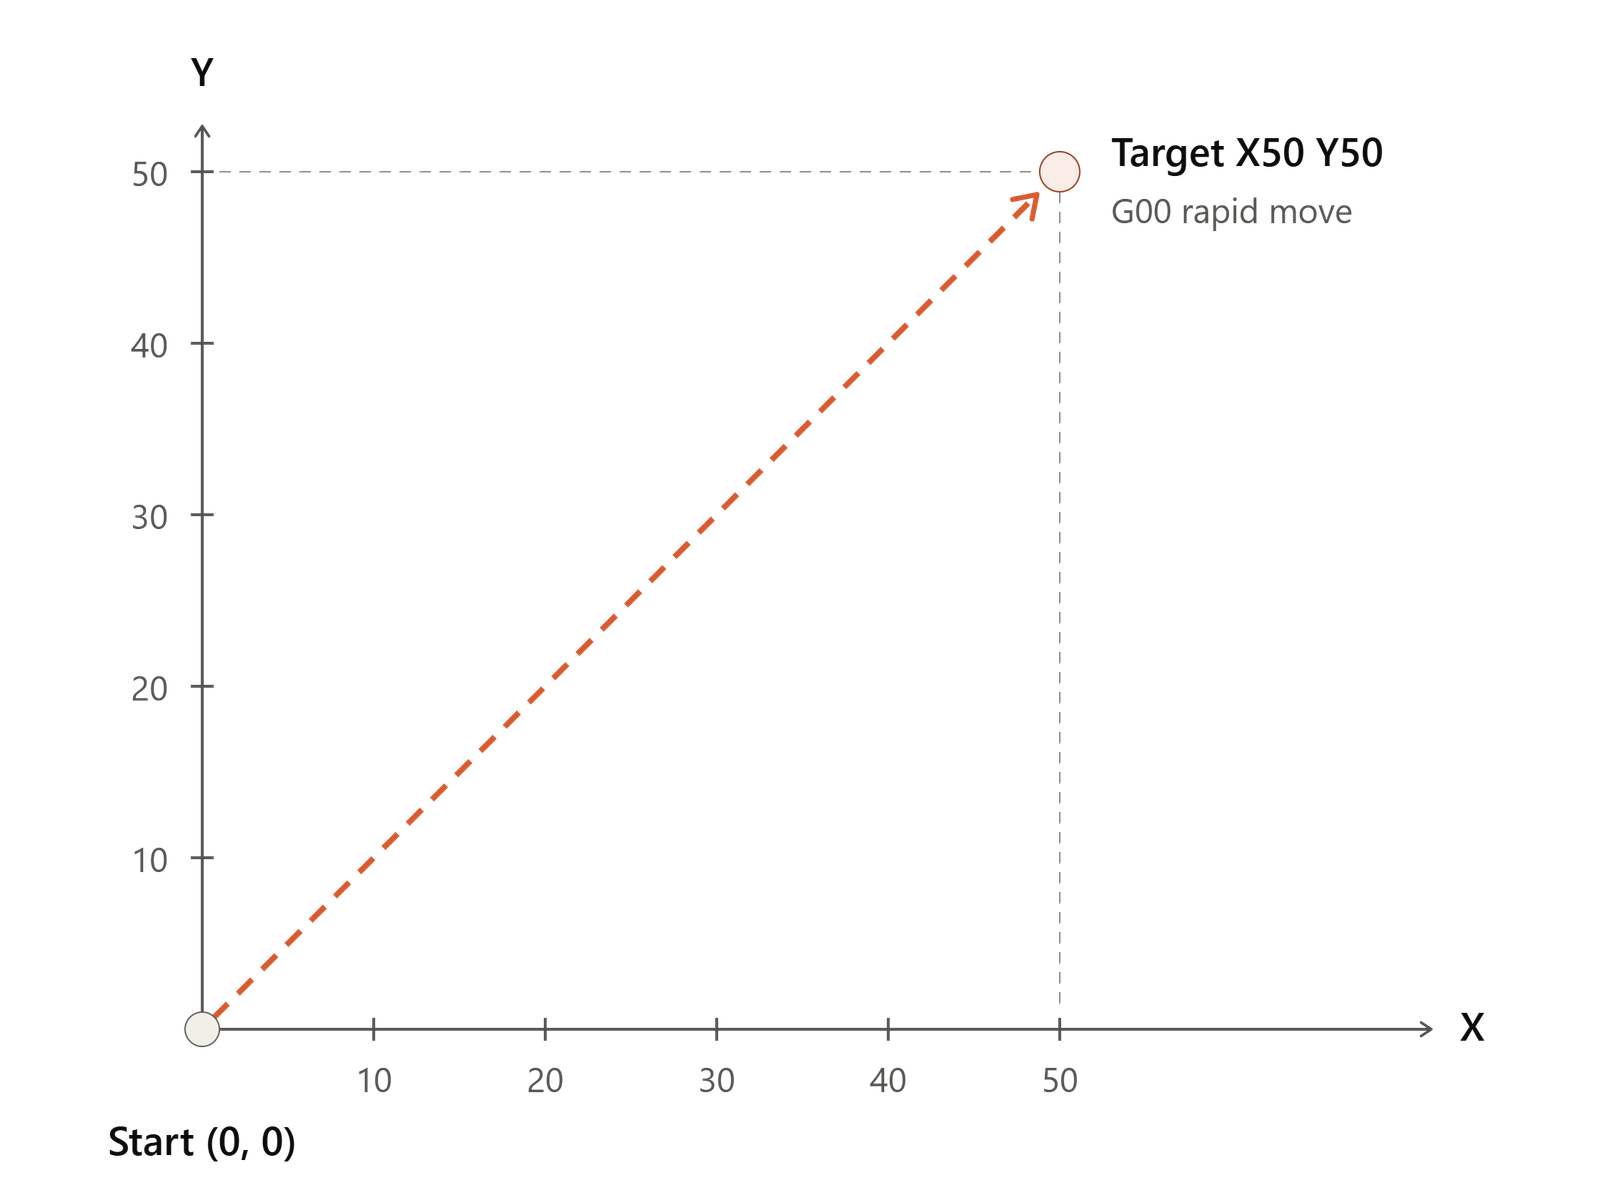
N50 G00 X0.0 Z2.0
N60 G74 R1.0
N70 G74 X0.0 Z-60.0 Q10000 F0.15
N80 G00 X150.0 Z150.0 M09
N90 M30
O0001 — G74 PECK DRILLING EXAMPLE
N10 G21 G99 — Metric units; feed in mm/revolution
N20 T0505 M06 — Select drill tool, tool offset 05
N30 G97 S800 M03 — Spindle ON
N40 M08 — Coolant ON
N50 G00 X0.0 Z2.0 — Rapid move to start position on center line
N60 G74 R1.0 — Retract amount of 1.0 mm for chip breaking
N70 G74 X0.0 Z-60.0 Q10000 F0.15 — Drill to Z-60 depth with 10mm pecks
N80 G00 X150.0 Z150.0 M09 — Rapid away and coolant OFF
N90 M30 — End and reset program