CNC External Turning and Radius Programming Guide
When we make a radius (R) on a corner or edge while cutting on the outside of a job, it is called Outside Turning with Radius. This process eliminates the sharp corners of the job.
Example of a Simple CNC Program
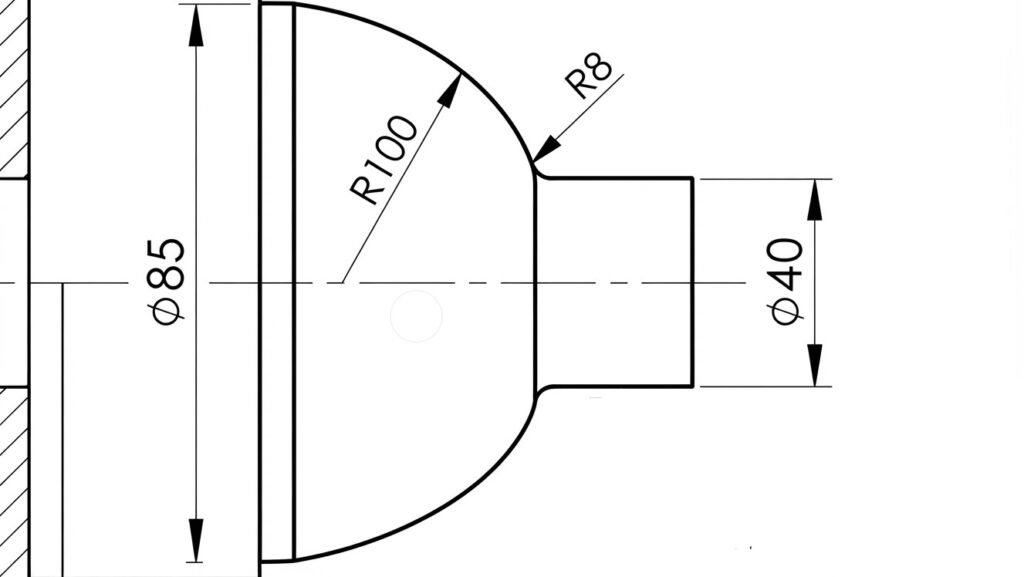
Description: Outside profile turning operation featuring straight cuts, an R8 mm fillet, and an R100 mm large curve.
O1005 (OUTSIDE PROFILE - R8 AND R100)
N10 G21 G99
N20 G50 S2000
N30 G96 S150 M03
N40 T0101
N50 G00 X40. Z2.
N60 G01 Z-25. F0.15
N70 G02 X56. Z-33. R8.
N80 G03 X85. Z-60. R100.
N90 G01 Z-75.
N100 G00 X100. Z10.
N110 M30
Code Explanation
O1005 (OUTSIDE PROFILE – R8 AND R100)
Program number definition. The text in parentheses is a comment describing the operation.
N10 G21 G99
G21: Sets the programming units to metric (millimeters).
G99: Sets the feed rate mode to Feed per Revolution (millimeters per rev).
N20 G50 S2000
Sets a maximum spindle speed limit of 2000 RPM to prevent the spindle from spinning dangerously fast as the cutting diameter decreases during Constant Surface Speed mode.
N30 G96 S150 M03
G96: Activates Constant Surface Speed (CSS) mode at 150 m/min.
M03: Turns the spindle ON in the clockwise (forward) direction.
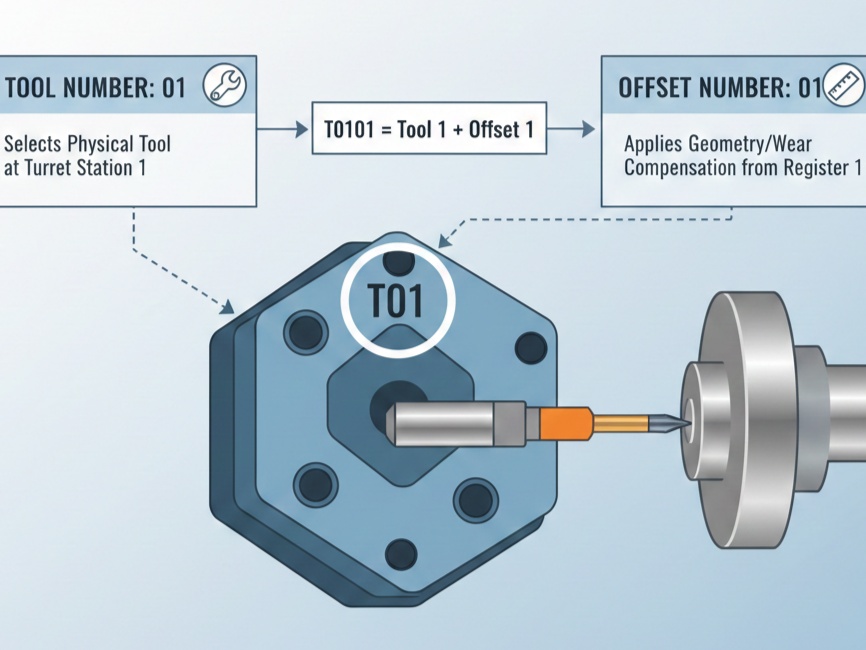
N40 T0101
Selects Tool 1 (T01) and applies its corresponding geometry/wear offset 1 (01).
N50 G00 X40. Z2.
Rapid traverse (G00) movement positioning the tool safely near the workpiece at X = 40.0 mm diameter and Z = 2.0 mm clear of the face.
N60 G01 Z-25. F0.15
Linear cutting move (G01) straight along the length to Z = -25.0 mm at a feed rate of 0.15 mm/rev.
N70 G02 X56. Z-33. R8.
Clockwise circular interpolation (G02) to machine an R8 mm radius fillet curve ending at X = 56.0 mm and Z = -33.0 mm.
N80 G03 X85. Z-60. R100.
Counter-clockwise circular interpolation (G03) to machine a large R100 mm curve transitioning up to X = 85.0 mm and Z = -60.0 mm.
N90 G01 Z-75.
Linear cutting move (G01) continuing straight down the cylinder to Z = -75.0 mm at the current diameter (X = 85.0 mm).
N100 G00 X100. Z10.
Rapid traverse (G00) retracting the tool safely away from the finished part to X = 100.0 mm and Z = 10.0 mm.
N110 M30
End of program and memory reset, stopping the spindle and coolant, and returning the program pointer to the beginning.
When a radius is to be given at the corner of a job, G02 (outside radius or clockwise) or G03 (inside radius or counterclockwise) is used. The parameter R is used for the radius.